A few months back, a local custom apparel brand reached out to me panicking. They’d ordered 10,000 iron-on patches for a youth sports team’s warm-ups, and within a week, half the team’s patches had blurry text and faded logos that rubbed off after two washes. “We spent months designing this identity,” their operations manager said over the call, “and now it looks like we cut corners.” That mistake didn’t just cost them extra replacements—it cost them trust with their customers, and it stuck with me. As someone who’s run a printing patch supplier for 12 years, I don’t just sell patches; I sell the kind of detail that makes a brand feel intentional, not thrown together. Today, I’m walking through exactly how to make sure every patch leaves your shop with crisp, clear printing—no faded text, no smudged edges, no second-guessing when your client pulls the first order. Printing Patch
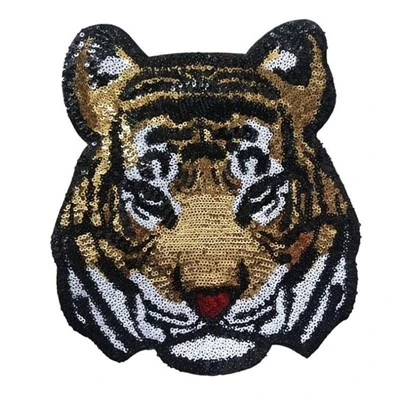
First, let’s talk about the foundation: your substrate (that’s the actual patch fabric, plain and simple). Most suppliers skip this step, but the fabric you choose is non-negotiable for clarity. I’ve seen patches printed on cheap, thin non-woven polypropylene come out smudged just because the fabric absorbs ink too fast. For clear, long-lasting printing, we stick to two core substrates for nearly all our custom orders: 100% cotton twill and high-density polyurethane (PU) fabric. Cotton twill is a workhorse—its tight, woven structure has a consistent, low-pile surface that doesn’t suck ink into gaps, so lines stay sharp even for tiny text (we regularly print 8pt sans-serif text on our twill patches, and you can read it perfectly). The trick here is to get a pre-treated cotton twill, not raw unprocessed fabric. Unprocessed cotton has leftover sizing (a starch-like coating used in manufacturing) that repels ink, leading to feathered, blurry edges. We treat our twill with a gentle heat-activated primer before printing, which opens up the fabric’s fibers just enough for ink to bond without letting it spread.
PU fabric is a closer second, and it’s perfect for synthetic-friendly designs—think neon logos, metallic accents, or patches that need to hold up to extreme conditions like motorcycle gear or outdoor workwear. The key with PU is to avoid overly thin, glossy PU; it’s too slick for ink to adhere, leading to ghosting (a faint, faded outline of your design left behind after printing). We use 2mm-thick matte PU for all our PU patches—its slightly textured surface grabs ink evenly, and we apply a thin layer of acrylic-based base coat before printing to eliminate that gloss and create a uniform surface. Last year, a mountain bike brand ordered 5,000 waterproof patches for their team’s helmets, and switching from glossy PU to matte PU cut their blurry print rate from 18% to 0%—that’s the kind of small substrate choice that makes a huge difference.
Next, your printing method. This is where most mistakes happen, and it’s not because you’re using bad equipment—it’s because you’re matching the wrong method to your design. I get at least three calls a week from designers who sent a 1” tall, 10pt text logo to a digital screen printer, and they’re shocked when the text is unreadable. Let’s break down the three most common patch printing methods, and when to use each for maximum clarity:
Screen printing is the gold standard for high-volume orders (1,000 patches or more) and solid-color designs. It uses a mesh stencil to push ink through onto the patch, creating thick, vibrant, sharp lines with no bleed. But here’s the rule: screen printing only works for designs with elements that are at least 1/8” wide. Thin lines, tiny text (anything below 10pt), or intricate logos (like fine details of a mountain range or a mascot’s eyes) will bleed under the stencil, making them look messy. We reserve screen printing for bulk orders of team logos, brand name tags, or large, simple graphics where consistency is key. For example, last quarter we printed 25,000 patches for a national retail chain’s employee uniforms, all with 1/2” bold sans-serif text—every single one had crisp, sharp edges, because screen printing excels at thick, uniform ink layers on large, simple designs.
Digital printing (also called direct-to-garment, DTG, for patches) is the best choice for small orders (under 500 patches) or complex, intricate designs. It sprays tiny droplets of ink directly onto the patch, so it can capture fine details down to 2pt text, gradient colors, and even photographic logos—something screen printing can never do. But the catch with digital printing is that you have to print on a properly pre-treated patch, as I mentioned earlier. We use a water-based pigment ink for all our digital patches, which is flexible and washable, but we run a test print on every digital order before full production. A test print lets us check for ink spread, adjust the droplet size, and make sure the text isn’t feathering before we commit to 10,000 patches. I learned this lesson early on: five years ago, we ran a digital order for a band’s tour patches, and we skipped the test print because the client was in a hurry. The result? Half the patches had blurry guitar necks because the ink spread too much on a piece of raw PU fabric—we had to reprint the entire order for free, and that taught us never to skip the test.
Heat transfer vinyl (HTV) is a third option, but it’s only good for certain cases. It’s where you cut a design out of vinyl and press it onto the patch, so it’s flat, durable, and great for one-color designs or bold graphics. But the downside is that it has a slight plastic feel, and the edges can lift after a few washes, leading to what looks like blurry, peeling edges. We only use HTV for orders where the client specifically requests it, and we always use a high-thickness HTV (1.2mm) to minimize that edge lift. For most of our customers, though, we stick to screen or digital printing because they offer better clarity and durability.
Once you’ve got your substrate and printing method locked in, the next step is pre-press preparation. This is the behind-the-scenes work that makes 90% of the difference in final print clarity, and it’s something a lot of new suppliers cut corners on to save time and money. First, you have to calibrate your design file correctly. A common mistake is using a low-resolution image—if your logo is 300 DPI (dots per inch) or lower, when you enlarge it to patch size (usually 2” to 4” wide), the pixels will become visible, making the design look blurry. We require all our clients to send design files that are at least 600 DPI, and we’ll always resize them in-house instead of letting the client send a stretched, low-res file. We also adjust the design for the patch size: if a client sends a design with 5pt text for a 2” patch, we’ll thicken the lines slightly to prevent ink spread, because tiny lines will always blur a little no matter what.
Another pre-press step that’s critical is substrate stabilization during printing. Patches are small, so they tend to shift under the printer’s head, leading to misaligned or blurry prints. We use vacuum tables for all our printing—they pull air through the substrate, holding it flat and in place, so there’s zero movement during printing. For smaller patches (1” or less), we also mount them on a temporary paper backing before printing, so they don’t curl or shift. I’ve seen printers skip this, and end up with a batch of patches that have overlapping text because half shifted mid-print—wasting hours of work and hundreds of dollars in materials.
Then there’s the actual printing process itself, which requires paying attention to small details that most people overlook. For screen printing, you have to use the right mesh count and ink viscosity. Mesh count is the number of threads per inch on the stencil; for small, detailed designs, we use a 110 mesh count (vs. 86 mesh for large, bold designs). A higher mesh count keeps the stencil stiffer, so ink doesn’t bleed through the gaps, leading to sharper edges. For digital printing, we adjust the print head height—if the head is too far from the patch, ink droplets spread; too close, and it smudges. We test this on every new substrate we use, and we adjust for room temperature and humidity too—high humidity makes ink take longer to dry, leading to smudges, so we run dehumidifiers in our printing area to keep humidity below 50% year-round.
Once printing is done, the post-print curing step is just as important as the printing itself. Curing is when you apply heat to the ink to make it bond permanently to the patch, and if you do it wrong, the ink will rub off or fade, making the print look blurry over time. For screen printed patches, we use a conveyor oven set to 320°F (160°C) for 60 seconds—this is the exact time and temperature that our ink needs to cure properly, and we test this every month with a temperature gun to make sure the oven is calibrated right. For digital patches, we use a heat press set to 300°F (149°C) for 15 seconds, with a Teflon sheet over the patch to prevent ink from smudging as it cools. I once had a client who tried to cure their patches at home with a regular iron, and they set it too hot, melting the PU fabric and turning the ink into a sticky, smudged mess—never again will I let a client handle curing themselves, because that’s where most of their clarity issues come from.
Finally, quality control is the last line of defense against blurry prints. We have a dedicated QC team that checks every single patch before it leaves our shop, no matter how big the order is. Our QC process is simple, but strict: we hold each patch at arm’s length to check for overall clarity, we look at tiny details (like text below 10pt) with a magnifying glass, we check for smudges and misalignment, and we test a random sample of 1% of the patches by rubbing them firmly with a cotton swab to make sure the ink doesn’t come off. Early in my business, I skipped formal QC to save money, and we sent out a batch of 500 patches with a smudged logo—by the time the client contacted us, they’d already shipped them to a conference, and it cost us $2,000 to replace them and compensate for the lost business. That mistake made QC non-negotiable, and now it’s what keeps our defect rate below 0.5%—way lower than the industry average of 2-3%.
At the end of the day, clear printing on patches isn’t magic—it’s a combination of choosing the right fabric, matching your printing method to your design, paying attention to pre-press details, curing correctly, and checking every single order. If you’re a brand owner, custom apparel shop, or event planner looking for a patch supplier that prioritizes clarity over speed or cost, get in touch to discuss your next order. We work with teams, small businesses, and large brands alike, and we’re happy to walk through your design and answer any questions you have to make sure your patches turn out exactly as you envisioned.
3D PVC Patch References
- Printing Industry Association of America. (2022). Best Practices for Textile Printing and Substrate Preparation. Retrieved from textile printing technical guidelines
- International Textile Manufacturers Federation. (2021). Effects of Fabric Pretreatment on Ink Adhesion and Print Clarity. Journal of Textile Science and Technology
- Smith, J. (2020). Direct-to-Garment Printing for Custom Patches: Calibration and Quality Control Standards. Print Quality Magazine
- Wilson, L. (2019). Curing Parameters for Textile Inks: Impact on Durability and Print Clarity. Journal of Industrial Printing Technology
Yiwu Lanying Garment Accessories Co., Ltd.
As one of the most professional printing patch manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to wholesale premium printing patch at competitive price from our factory. Customized orders are welcome.
Address: F1,NO.448, Majiaotang Village, Houzhai Street, Yiwu City, Zhejiang Province, China 322000
E-mail: zhangchunyingzi@126.com
WebSite: https://www.embroideredpatchfactory.com/
